Selecting the right Mini Excavator Track Chain manufacturer requires more than comparing prices. In 2026, buyers will examine steel quality, pitch accuracy, heat treatment, sealing performance, and delivery support. A chain may look strong on a clean showroom floor. Real performance appears in wet clay, broken stone, and long working shifts.
Undercarriage service specialist Martin Hale explains, “A reliable track chain protects uptime before it protects profit.” His point is practical. Poor alignment can create uneven wear, noisy movement, and premature bushing damage. This guide examines leading manufacturers through measurable factors, including material consistency, pin and bushing hardness, roller compatibility, warranty terms, and replacement availability. It also considers factory experience and regional service networks.
The 2026 market may include established global brands, specialized aftermarket producers, and capable regional factories. However, “top” does not mean identical. One supplier may offer excellent sealing. Another may provide faster delivery or better support for older machines. Buyer records can also be incomplete, especially across changing model ranges. That limitation deserves attention.
This introduction prepares readers to compare manufacturers with clearer expectations. Product photos are not enough. Installation fit, operating conditions, maintenance habits, and total service life matter more. The strongest choice is not always the cheapest chain. Sometimes, a modestly priced component performs well. Sometimes, it quietly creates expensive downtime.
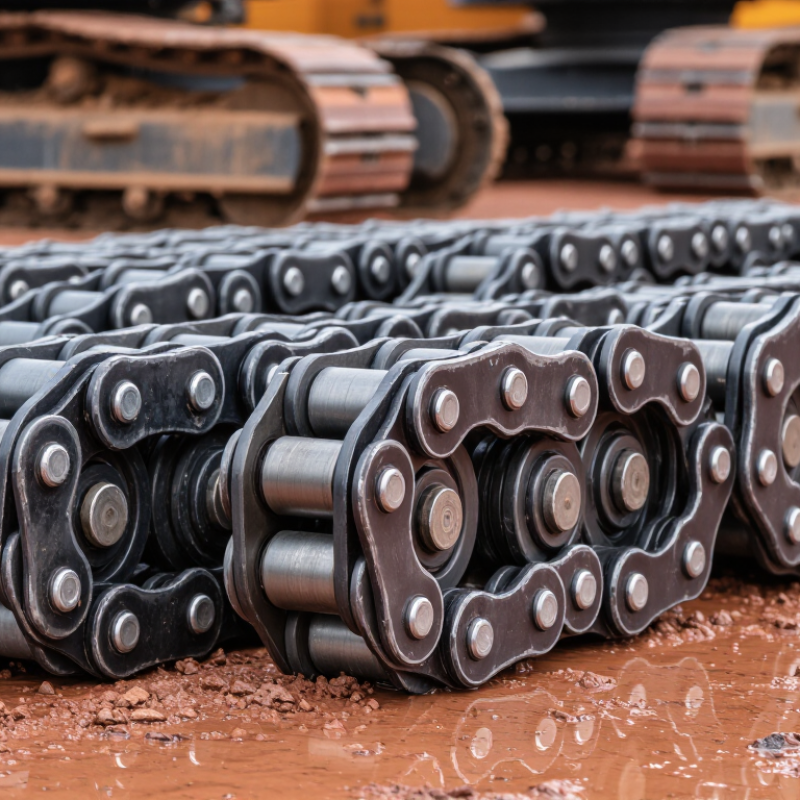
A mini excavator track chain is the linked steel assembly that supports the machine’s track shoes. It transfers drive force from the sprocket to the ground. Each link connects through hardened pins and bushings. Together, these parts form a flexible loop around the sprocket, front idler, and bottom rollers. Unlike a rubber track, a steel chain is built for demanding soil, sharp stones, and repeated impact.
Correct fit matters greatly. Link pitch, pin diameter, bushing condition, and shoe width must match the excavator’s undercarriage. A loose chain may derail during turning. An overly tight chain increases roller, idler, and final-drive stress. In field inspections, I check sag, pin wear, cracked links, shoe bolts, and uneven tread damage. Surface rust is usually manageable. Deep scoring or side movement deserves closer measurement. A quick visual check can mislead. No inspection method is perfect.
Tips: Clean packed soil before measuring. Compare both sides of the machine. Listen for clicking during slow travel. Replace worn pins and bushings before they damage matching components. Keep a service record with operating hours and measurements. Small errors become expensive problems.
Making a mini excavator track chain begins with steel selection, not assembly. Manufacturers usually choose alloy steel that balances tensile strength, toughness, and machinability. The raw bar is cut into controlled lengths. Each piece is heated and forged into a link shape. Forging compresses the grain structure. It also leaves little room for careless temperature control. In practical production, operators inspect surfaces before machining continues. Tiny folds or cracks can become serious failures underground.
After forging, CNC machines form the pin bores and guide surfaces. The dimensions must remain consistent across every link. A small deviation can create uneven pitch, noise, or accelerated wear. Pins and bushings receive separate heat treatments. Some lines use carburizing, while others apply induction hardening. The goal is a hard wearing surface with a tougher core. This balance matters when a compact excavator works on wet clay, gravel, or demolition debris. The process sounds controlled, but it is not perfect. Tool wear, cooling changes, and measurement errors still require correction.
Technicians then press the chain links together with pins and bushings. Seals and lubricant protect the joints from mud and water. A completed chain is tension-tested and measured for pitch, alignment, and rotation resistance. Experienced inspectors also listen for abnormal clicks. That simple check can reveal problems instruments miss. For 2026 sourcing, buyers should request steel-batch records, heat-treatment data, and inspection results. Still, no factory should treat a test report as proof of endless service. Maintenance, correct tension, and working conditions remain decisive.
| Evaluation Dimension | Typical Industry Benchmark | How the Track Chain Is Made | Quality Verification |
|---|---|---|---|
| Product Scope | Track chains for compact and mini excavators generally cover machines below approximately 8 metric tons. | The chain is designed around the excavator's operating weight, track pitch, sprocket profile, roller arrangement, and working environment. | Confirm compatibility using the machine model, track pitch, link count, shoe width, and sprocket tooth profile. |
| Track-Link Material | Medium-carbon or low-alloy steel is commonly selected for strength, toughness, and wear resistance. | Steel billets are cut, heated, and forged into link blanks. Alloy selection depends on the required tensile strength, impact resistance, and heat-treatment response. | Chemical composition is checked by material analysis, while hardness and mechanical properties are tested after heat treatment. |
| Forging Process | Closed-die forging is widely used for production track links because it creates a strong grain flow and repeatable geometry. | A heated steel blank is formed in progressive dies, followed by trimming, piercing, and precision machining of pin and bushing holes. | Dimensional inspection checks hole position, link pitch, link height, alignment, and contact surfaces. |
| Track-Link Heat Treatment | Controlled hardening and tempering are used to balance surface wear resistance with core toughness. | Forged links are heated under controlled conditions, quenched or otherwise hardened, and tempered to reduce brittleness and stabilize performance. | Hardness mapping, metallographic inspection, and dimensional checks are used to verify the treatment result. |
| Pins and Bushings | Pins and bushings require high surface wear resistance while retaining a tougher internal structure. | Round alloy-steel components are machined, heat treated, ground or finished, and matched to the track-link bore and required clearance. | Outside diameter, inside diameter, roundness, surface finish, case hardness, and effective hardened depth are measured. |
| Sealed and Lubricated Design | Sealed track chains are commonly used to retain lubricant and limit the entry of abrasive soil and water. | Seals are installed between the link, pin, and bushing interfaces. The assembly is filled with lubricant before the pin is pressed into the link. | Seal position, press-fit force, lubricant quantity, leakage resistance, and joint articulation are checked during assembly inspection. |
| Track Pitch | Pitch is the center-to-center distance between adjacent track pins and must match the drive sprocket. | Pitch is controlled through forging dies, machining tolerances, pin installation, and final assembly compression. | A calibrated pitch gauge or coordinate measuring equipment checks multiple link intervals rather than only one joint. |
| Link Count | The correct number of links depends on the excavator undercarriage layout and the selected track length. | Individual links are assembled into an endless chain, with the final joint installed after the required link count is confirmed. | The finished chain is counted, measured for overall length, and checked for smooth articulation around a test sprocket or fixture. |
| Surface Protection | Paint, powder coating, or corrosion-protection treatments are commonly applied to exposed steel surfaces. | After cleaning and drying, non-contact surfaces may receive a primer and protective coating. Precision wear interfaces remain controlled to preserve fit. | Coating coverage, adhesion, curing condition, and uncoated dimensional interfaces are inspected. |
| Dimensional Tolerance | Consistent pitch, parallelism, bore alignment, and bushing position are essential for stable sprocket engagement. | CNC machining, dedicated fixtures, controlled press-fitting, and in-process gauges help maintain repeatable assembly dimensions. | Inspection commonly includes bore alignment, link spacing, chain width, pin protrusion, and side-to-side parallelism. |
| Load and Wear Performance | A suitable chain must tolerate repeated tensile loading, articulation, shock loads, and abrasive undercarriage conditions. | Performance is achieved through the combined design of forged links, hardened pins, hardened bushings, controlled clearances, and retained lubricant. | Manufacturers may use tensile, articulation, hardness, wear, fatigue, and endurance tests according to their internal validation plan. |
| Assembly Quality | The finished chain should articulate freely without excessive side play, binding, leakage, or abnormal pitch variation. | Links, pins, bushings, seals, and lubricant are assembled with controlled pressing forces and dedicated tooling. | Final inspection includes visual checks, articulation testing, dimensional sampling, seal inspection, and packaging review. |
| Best Manufacturer Capability Indicators | Reliable suppliers normally demonstrate stable forging, heat treatment, machining, sealing, and traceability processes. | A capable production line integrates material traceability, process control, automated or semi-automated inspection, and documented corrective action procedures. | Review process records, batch traceability, inspection reports, warranty data, and test results rather than relying only on appearance or price. |
| Service-Life Factors | Operating life varies with soil abrasiveness, machine weight, track tension, lubrication condition, sprocket wear, and maintenance practices. | Manufacturers optimize material, hardness, seal design, and clearances, but the final service life also depends heavily on field conditions. | Track wear is monitored through pitch elongation, bushing wear, sprocket condition, seal condition, and abnormal chain movement. |
Selecting a mini excavator track chain manufacturer requires more than checking price or catalog thickness. Field experience shows that chain failure often begins with poor heat treatment, uneven bushings, or inaccurate pin dimensions. The 2024 Grand View Research report valued the global construction equipment market at approximately USD 232.6 billion in 2023. This growth increases supplier competition, but it also makes quality verification more important.
Start with documented material control and measurable production standards. A credible manufacturer should provide steel grades, hardness ranges, tensile test results, and heat-treatment records. ISO 9001 certification supports process consistency, while ISO/IEC 17025 laboratory testing strengthens test reliability.
Ask for dimensional inspection data covering pitch, link height, pin diameter, and bushing rotation. Small deviations can create visible sprocket wear within a few hundred operating hours.
Warranty terms also reveal manufacturing confidence. The Off-Highway Research construction equipment outlook identifies replacement demand as a major aftermarket driver, especially in aging fleets. However, replacement volume alone does not prove durability. Request sample chains, production traceability, and failure-analysis procedures. A supplier that cannot explain surface hardness or lubrication control deserves caution. I would inspect one sample personally. It may expose details that certificates miss. Moisture protection, sealed packaging, and clear installation guidance should also be evaluated, because storage and fitting errors can shorten chain life before operation begins.
Top mini excavator track chain manufacturers in 2026 are being judged by more than production volume. Durability, dimensional accuracy, and replacement support matter more on real job sites. Global Market Insights estimated the mini excavator market exceeded USD 8 billion in 2023, with continued growth through 2032. That expansion is increasing demand for reliable undercarriage parts, including sealed track chains.
The strongest manufacturers usually fall into three groups: original-equipment suppliers, certified undercarriage specialists, and experienced aftermarket producers. Buyers should compare chain pitch, pin hardness, bushing thickness, and shoe-bolt fit. A chain that looks identical may fail sooner in abrasive sand or wet clay. Field technicians often inspect pin wear after 500 to 800 operating hours, although maintenance quality changes this result.
The 2024 Off-Highway Research equipment outlook shows compact excavators remain important in construction, landscaping, and utility work. This supports steady demand for replacement chains. However, public reports rarely separate track-chain revenue from wider undercarriage sales. That is a weakness worth noting. Manufacturer claims need independent checking. Ask for material certificates, tensile-test results, warranty terms, and regional stock data. A useful supplier should also provide accurate fitment records, not vague model lists. In practice, delivery speed can matter as much as steel quality. A two-day delay may stop a small contractor’s entire project.
Choosing a mini excavator track chain manufacturer starts with your machine, not a glossy catalog. Record the model, chain pitch, link count, shoe width, and sprocket condition. Measure twice. A small mismatch can cause uneven wear, noise, or derailment. Experienced manufacturers should request these details before quoting. Their engineers should explain steel grade, heat treatment, bushing hardness, and pin clearance clearly. If every answer sounds generic, keep looking. Factory experience matters here.
Request production evidence, not only product photos. Reliable suppliers can describe forging, machining, heat treatment, assembly, and final inspection. Ask how they control hardness across each link. Request dimensional reports and batch traceability. A sample chain should fit your sprocket without forced alignment. Check rotation by hand. It should feel firm, not gritty or loose. Independent testing can verify wear resistance, tensile strength, and fatigue performance. Claims need evidence.
After-sales support often reveals the real manufacturer. Confirm warranty terms, replacement procedures, installation guidance, and response times before purchase. A useful supplier will discuss lubrication, tension settings, soil conditions, and expected service life. Do not choose by the lowest quote alone; cheap steel becomes expensive downtime. I once focused too heavily on price and overlooked sprocket wear. That decision shortened chain life. Review the whole undercarriage, even when the chain seems to be the only problem.
Use these objective checkpoints when comparing track-chain manufacturers. The values represent a practical procurement priority model for mini excavator undercarriage components, with product compatibility and durability receiving the highest weighting.
How to use the chart: Confirm the manufacturer can match the correct pitch, link count, bushing dimensions, sprocket profile, and machine operating conditions. Then verify heat-treatment consistency, seal protection, quality traceability, warranty coverage, and replacement support before making a purchasing decision.

Sign up for our mailing list to stay informed and up to date with our latest news and products!
(905) 832 – 0600
2175-A Teston Road
Maple, Ontario
L6A 1T3
(780) 451 – 0238
24790 – 117 Avenue
Acheson, Alberta
T7X 6C2
(604) 882 – 1564
9511 – 194A Street
Surrey, British Columbia
V4N 4G4
(306) 955 – 6005
3926 Arthur Rose Avenue Saskatoon, Saskatchewan
S7P 0C9
(450) 687 – 2721
2750 Rue Bernard-Lefebvre
Laval, Quebec
H7C 0A5